Leave Your Message
Engineered for high performance, durability, and maximum energy savings in harsh environments.
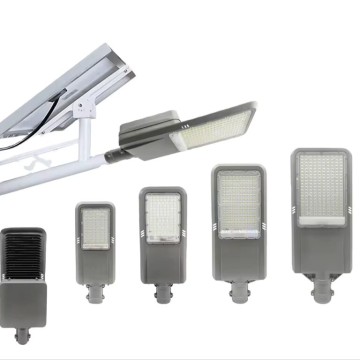
The United Kingdom's industrial landscape is undergoing one of the most significant transformations since the Industrial Revolution. Driven by the legally binding commitment to achieve Net Zero carbon emissions by 2050, UK enterprises are auditing their operations to eliminate energy waste. Industrial buildings, including massive distribution centers in the Midlands' "Golden Triangle," manufacturing facilities in the North East, and high-tech science parks in the South East, consume vast amounts of electricity. Lighting accounts for up to 40% of an average warehouse's energy bill. Consequently, high-performance LED high bay retrofits and new installations have shifted from simple facility upgrades to strategic financial and environmental priorities.
As a leading OEM LED High Bay Industrial Exporter & Factory, we design and produce luminaires that align perfectly with the UK's strict regulatory framework and demanding operating conditions. Our high bay systems are engineered to withstand the damp, cold climates of British winters while offering industry-leading luminous efficacy (up to 180 lm/W) to maximize energy savings and qualify for local green financing and tax incentives.
The UK commercial and industrial sector is unique, characterized by high energy tariffs, strict building regulations, and a rapid shift toward automated logistics. Several major trends are currently driving the specification of LED high bay lights across Great Britain and Northern Ireland:
With high labor and energy costs, UK facility managers are demanding intelligent lighting systems. The trend is moving away from "always-on" static lighting toward dynamic, sensor-controlled illumination. Our OEM LED high bays support DALI-2 (Digital Addressable Lighting Interface) and wireless protocols like Zigbee or Casambi. This allows for seamless integration with Building Management Systems (BMS), enabling occupancy sensing, daylight harvesting, and automated dimming schedules. In vast UK logistics hubs where aisles are only occupied sporadically, smart sensors ensure lights are active only when needed, dramatically extending luminaire lifespan and slashing operational costs.
Sustainability in the UK goes beyond energy efficiency. There is a strong push toward circular economy principles, championed by organizations like the Society of Light and Lighting (SLL) and CIBSE. Specifiers now look for modular LED high bays where drivers, LED boards, and optics can be easily replaced or upgraded without discarding the entire aluminum housing. Our factory prioritizes modular product architecture, offering UK partners fully serviceable high bay fixtures that reduce electronic waste and lower long-term maintenance overheads.
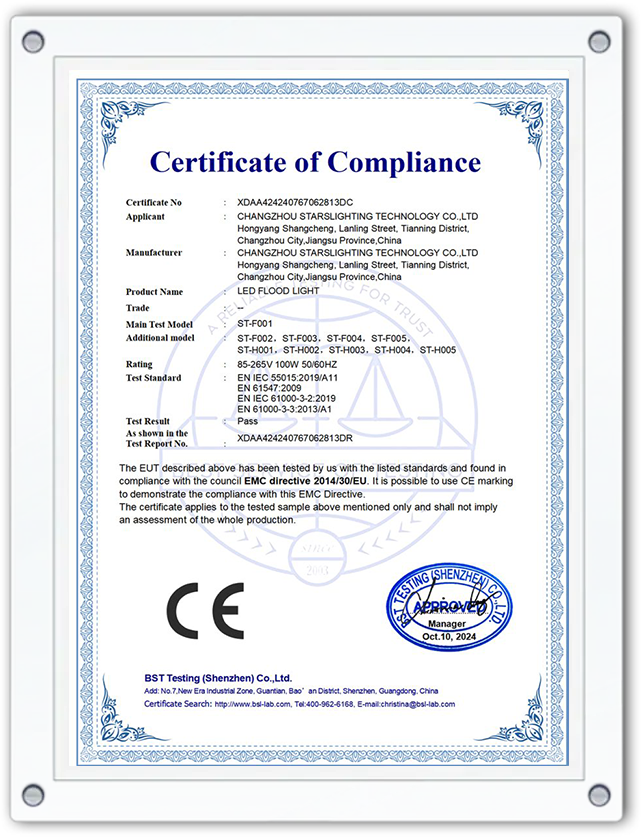
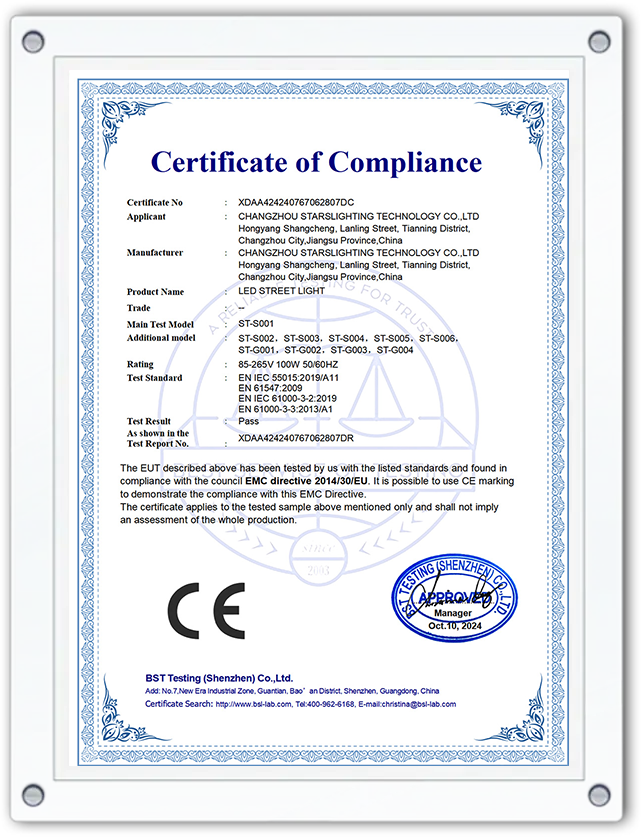
Following Brexit, the UKCA (UK Conformity Assessed) marking has become the mandatory product marking for goods placed on the market in Great Britain. Additionally, the updated Part L of the Building Regulations enforces stricter energy efficiency thresholds for non-domestic buildings. Our manufacturing lines are fully aligned with these updates, ensuring all exported LED high bays meet or exceed the minimum efficacy requirements, carry certified UKCA/CE markings, and comply with RoHS and WEEE directives.
Industrial spaces in the UK vary widely, each presenting distinct environmental challenges. Our OEM services allow us to customize optical distributions, thermal management, and ingress protection to suit these specific applications:
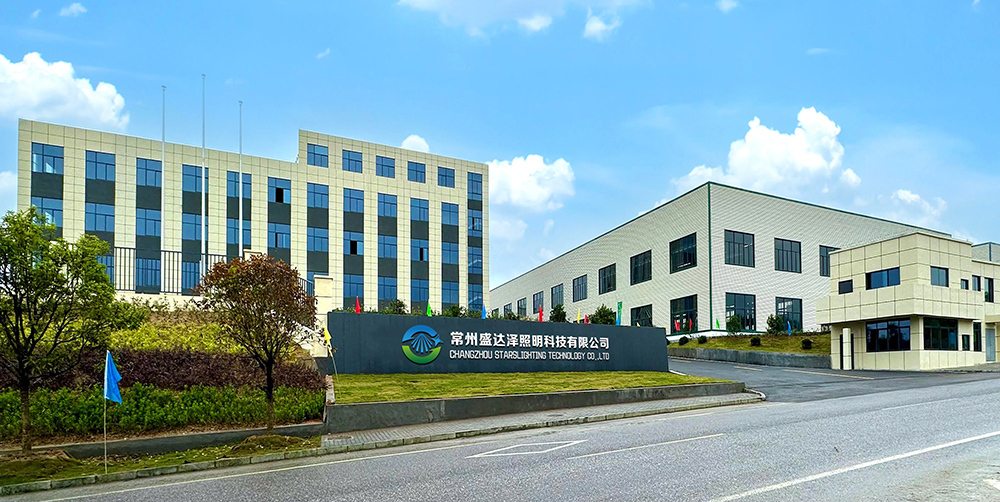
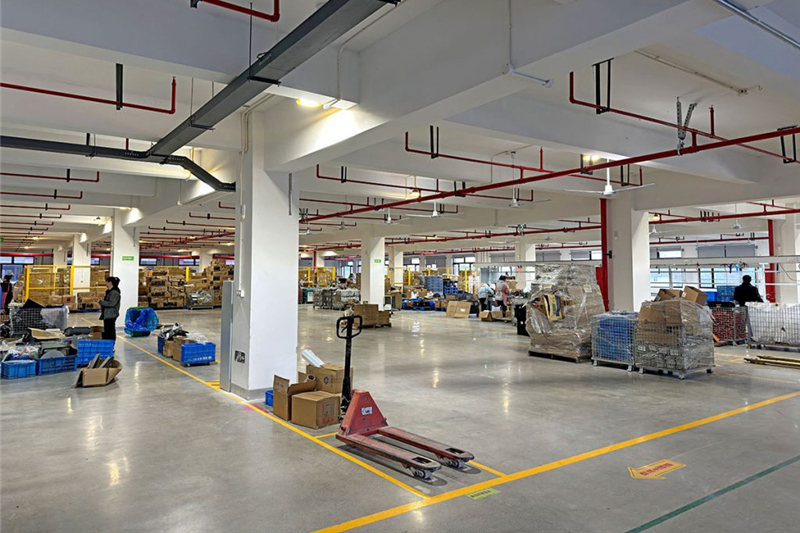
Established in 2016 and located in Hengshanqiao Town, Wujin District, Changzhou City, Jiangsu Province, Changzhou Starslighting Technology Co., Ltd. has grown into a premier manufacturer in the outdoor and industrial LED lighting sector. The factory currently has 80 employees, a building space of about 3,800 square meters, and an annual production capacity of up to 200,000 sets.
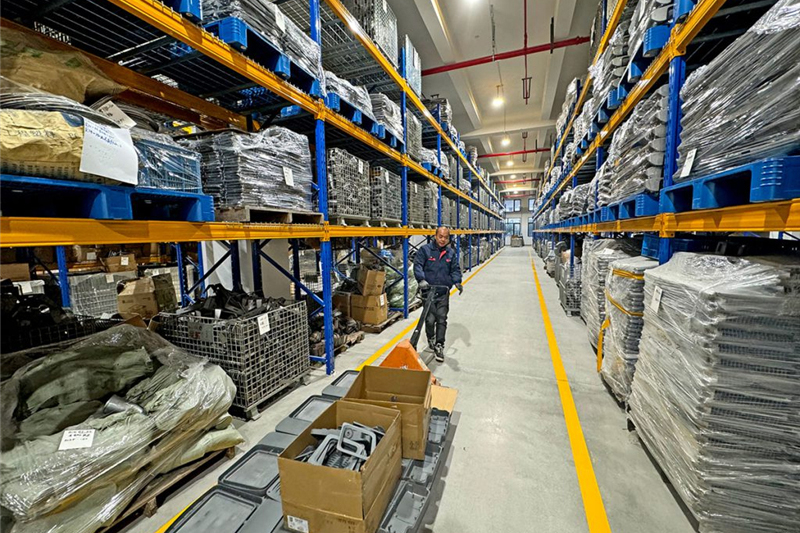
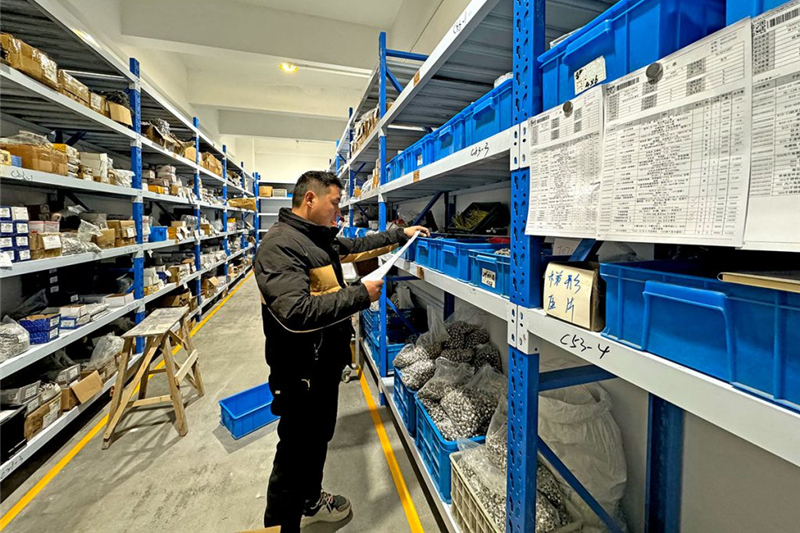
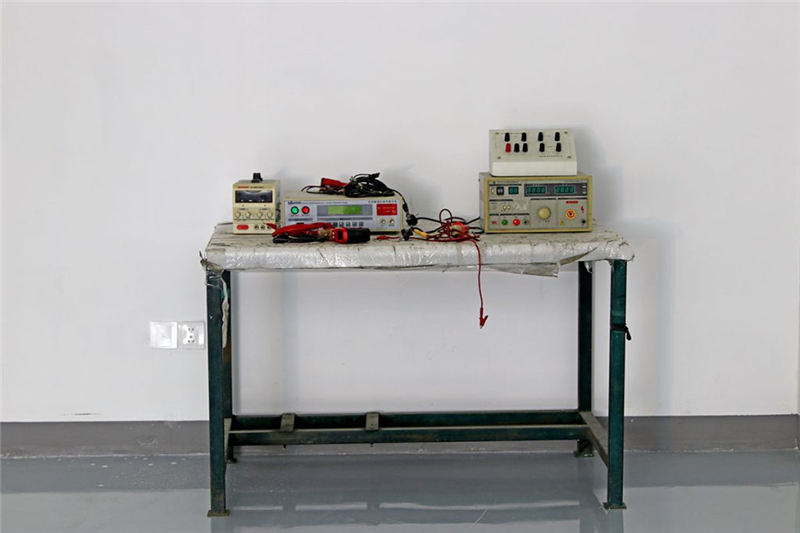
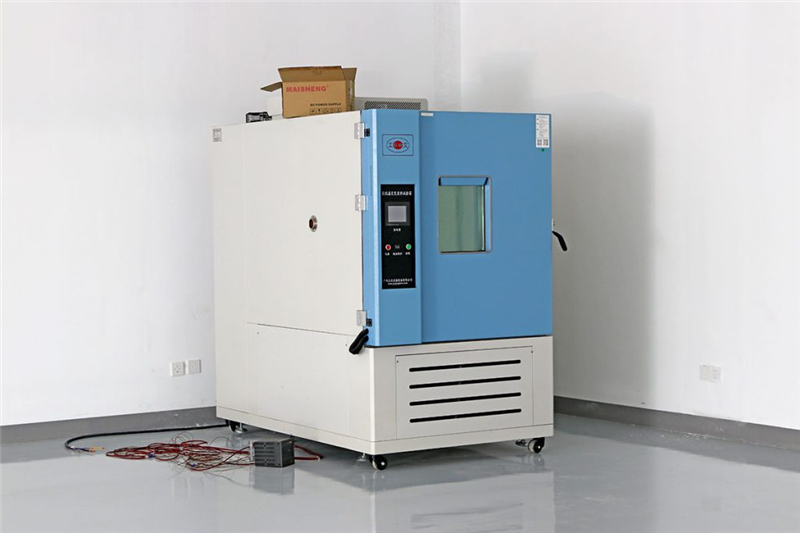
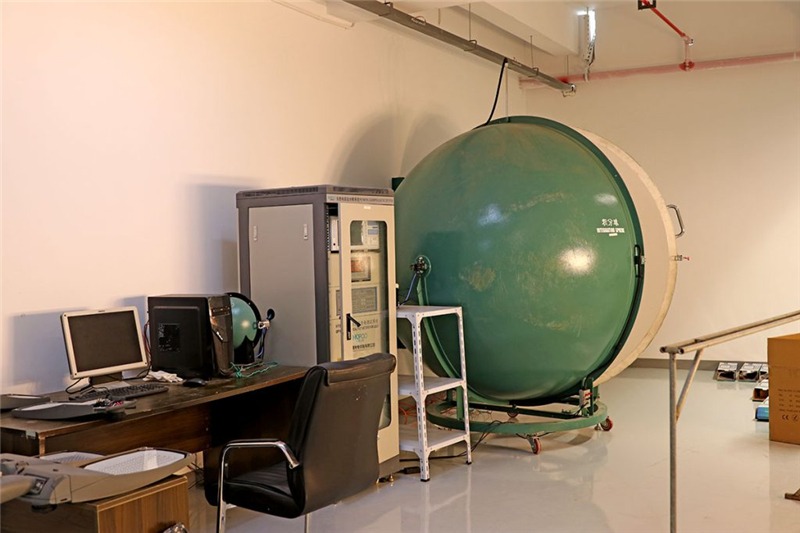
To better serve our international partners and expand into demanding markets like the United Kingdom, Starslighting Technology has established a dedicated technical team of 5+ members and a specialized after-sales service and quality control team of 3+ members. Focused on our core expertise in outdoor and industrial lighting products, we are equipped with professional testing and manufacturing facilities, including an integrating sphere, Distribution Photometric Darkroom, impact testing equipment, aging test chambers, and SMT pick-and-place machines.
Our complete production and quality management system, professional R&D and manufacturing team, first-class production equipment, and excellent after-sales service team have made Starslighting well-known in the outdoor and industrial lighting industry around the world.
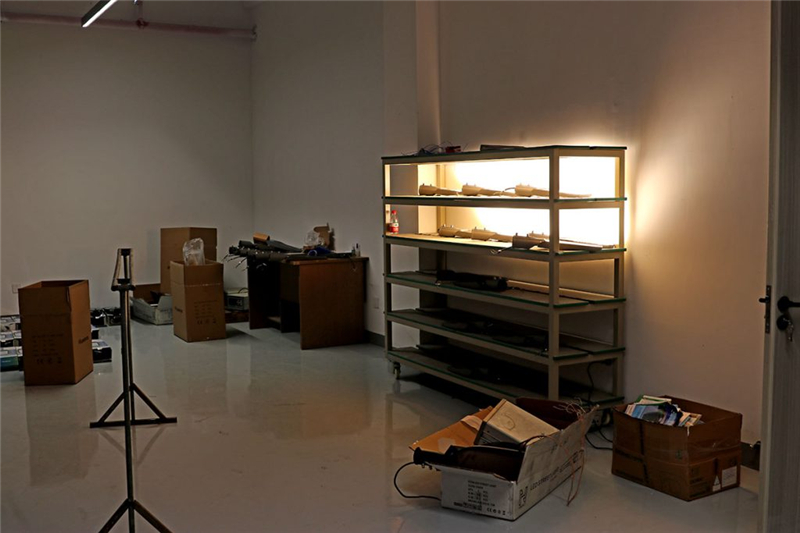
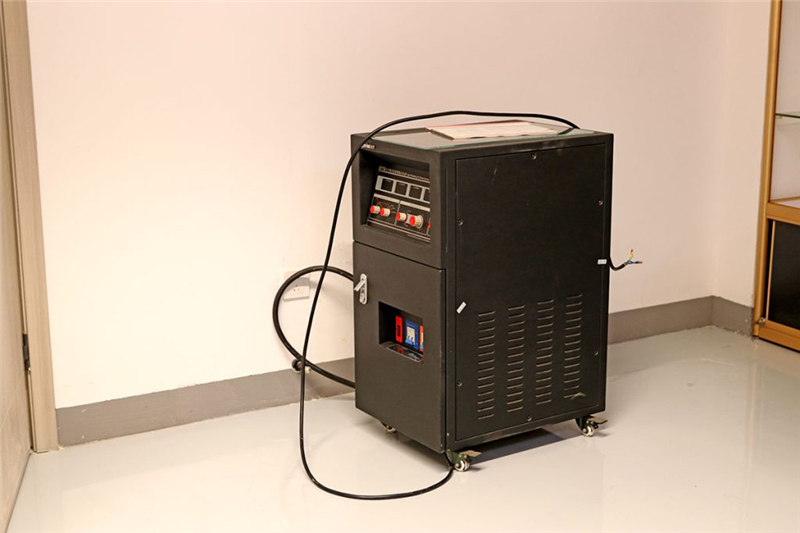
Starslighting has obtained CCC quality management system certification, as well as relevant international certificates such as CE, CB, RoHS, ERP, and ISO.
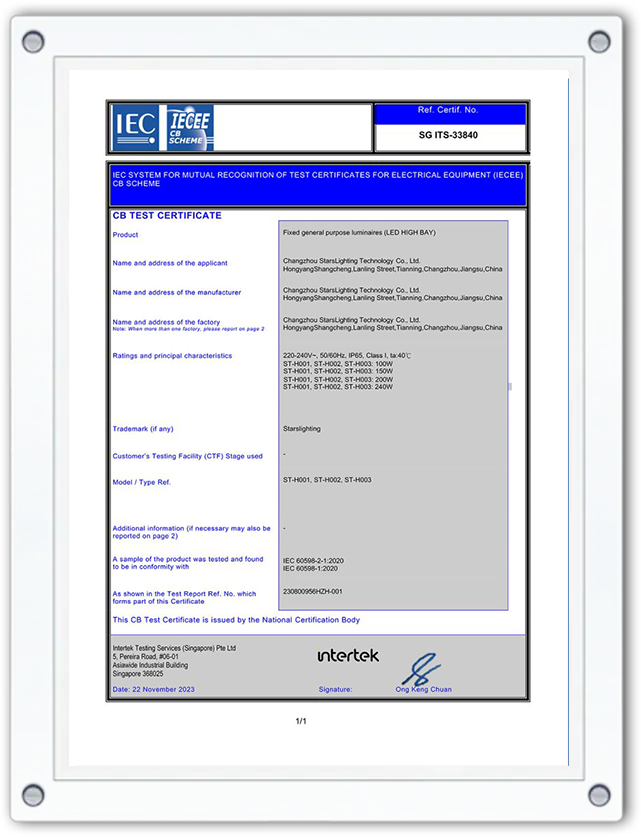
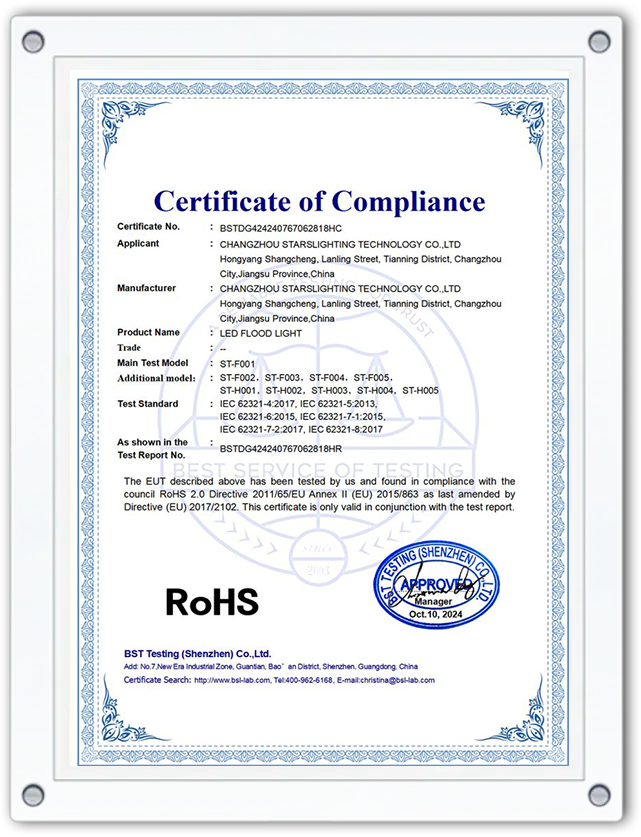
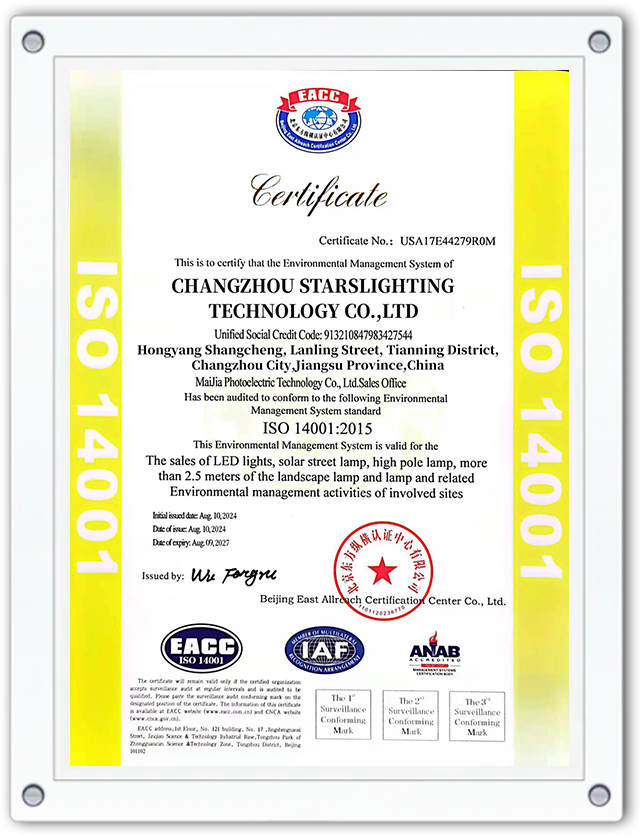
Our journey of innovation, quality, and global expansion in the LED lighting industry.
Explore our full range of high-efficiency LED solutions designed for UK municipal, commercial, and industrial applications.